The selection of isolation valves is a foundational engineering decision that dictates the safety, efficiency, and long-term economic viability of modern industrial infrastructure. Within the global valve market, which reached approximately USD 81.8 billion in 2024 and is projected to expand toward USD 126 billion by 2025 , the gate valve vs ball valve represent the two most dominant architectures for on/off service. While both serve the primary function of stopping or initiating flow, their mechanical ontologies—one defined by linear motion and the other by quarter-turn rotation—create distinct performance profiles across varying pressures, temperatures, and media types. This report provides an exhaustive technical comparison of these technologies, examining their design principles, hydraulic characteristics, regulatory compliance frameworks, and lifecycle economics through the lens of industrial expertise.
Gate valve vs Ball valve Mechanical Ontologies and Functional Principles
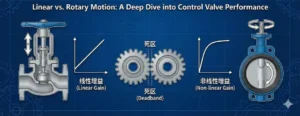
The fundamental difference between gate valves versus ball valves originates in their internal mechanisms for flow obstruction. A gate valve operates as a linear-motion device, where a flat or wedge-shaped closure element—the “gate”—moves perpendicular to the flow path. This design is often likened to a sliding door or a guillotine, where the gate is lifted or lowered by a threaded stem to clear or block the passage. In contrast, a ball valve utilizes a rotary-motion mechanism, employing a spherical disc with a bored center that rotates 90 degrees to align with or perpendicular to the pipeline.
Linear Motion Dynamics of Gate Valves
The mechanical advantage of the gate valve lies in its ability to provide a robust, straight-through flow path without the internal obstructions often found in globe or check valves. The gate is typically wedge-shaped to ensure that the final downward movement of the stem wedges the closure element tightly between the seats, enhancing sealing performance in high-pressure applications. This wedge-action design is particularly effective because the pressure of the fluid itself can assist in pushing the gate against the downstream seat, creating a more secure seal as pressure increases.
However, the linear motion requires multiple turns of the handwheel—often ranging from a dozen to over a hundred for large-diameter valves—to achieve a full transition from open to closed. This slow operation is an inherent characteristic that protects the piping system from hydraulic shock, but it limits the valve’s responsiveness in emergency scenarios where rapid isolation is critical. Furthermore, the sliding motion of the gate across the seats generates friction and wear, making the gate valve less suitable for frequent cycling than rotary alternatives.
Rotary Motion Dynamics of Ball Valves
Ball valves have gained immense popularity in natural gas systems and chemical processing due to their rapid quarter-turn operation. The 90-degree rotation allows for nearly instantaneous shutoff, which is indispensable for automated systems and emergency response. In a ball valve, the sealing surfaces are in constant contact or near-contact with the polished sphere, and the “wiping” action during rotation helps clear the seats of minor debris, a feature often referred to as a self-cleaning design.
There are two primary configurations for ball valves: floating and trunnion-mounted. In the floating ball design, common in smaller sizes and lower pressure classes, the ball is supported only by the seats, allowing it to “float” slightly downstream under pressure to seal against the downstream seat. In trunnion-mounted designs, required for larger diameters and higher pressures, the ball is fixed on a vertical axis by a support shaft (trunnion), and the seats are spring-loaded to move against the ball. This fixed-ball structure significantly reduces the operating torque and prevents the ball from shifting under extreme differential pressures.
| Feature | Gate Valve | Ball Valve |
| Motion Type | Linear (Up/Down) | Rotary (90°) |
| Operation Speed | Slow (Multi-turn) | Fast (Quarter-turn) |
| Position Indicator | Rising Stem (Visible) | Handle Alignment (Parallel/Perpendicular) |
| Sealing Motion | Sliding/Wedge Contact | Rotational/Wiping Contact |
| Space Requirement | High Vertical Clearance | Higher Horizontal (Handle) Clearance |
Regulatory Compliance and Industry Standards
The engineering of industrial valves is strictly governed by standards that define wall thickness, material properties, pressure-temperature ratings, and testing protocols. The selection between a gate and ball valve is often dictated by the specific standards mandated for the project, such as API 6D, API 600, or ASME B16.34.
API 6D: The Pipeline Standard
API 6D is the definitive specification for pipeline valves used in petroleum and natural gas transportation. It prioritizes full-bore designs to accommodate “pigging” operations—the insertion of inspection or cleaning devices into the line. A core requirement of API 6D is the zero-allowable-leakage standard for closure testing, which is primarily achieved through resilient (soft) seats in ball, plug, and gate valves. API 6D valves also mandate features like automatic cavity pressure relief to prevent trapped fluids from causing dangerous pressure build-up within the valve body.
API 600: Heavy-Duty Industrial Gate Valves
API 600 is a specialized standard for bolted-bonnet steel gate valves used in refineries and high-pressure, high-temperature industrial processes. It imposes stricter requirements than general standards, particularly regarding minimum wall thickness and material robustness, to ensure that valves can withstand severe thermal stresses without deformation. While API 6D focuses on pipeline safety and sealing integrity over long distances, API 600 emphasizes durability and long-term stability in harsh plant environments.
ASME B16.34: The Versatile Industrial Baseline
ASME B16.34 is a comprehensive standard that applies to a broad range of valve types across multiple industries. It is the authoritative source for determining maximum allowable working pressure at specific temperatures based on material groups. Unlike the zero-leakage focus of API 6D, ASME B16.34 permits trace leakage according to defined acceptance criteria, making it suitable for metal-to-metal seated designs that may not achieve a bubble-tight seal. Many industrial gate and ball valves are dual-certified to both ASME B16.34 (for pressure ratings) and API 600 or API 6D (for design and testing specifics) to ensure broad project compatibility.
| Standard | Primary Application | Key Emphasis | Typical Valve Type |
| API 6D | Pipeline Transmission | Full Bore, Pigging, Cavity Relief | Trunnion Ball, Slab Gate |
| API 600 | Oil Refineries | Thicker Walls, Material Strength | Wedge Gate Valve |
| ASME B16.34 | General Industrial / Power | Pressure-Temperature Ratings | Ball, Gate, Globe, Check |
Hydraulic Efficiency and Flow Characteristics
The hydraulic performance of a valve is quantified by its flow coefficient (Cv) and the pressure drop it induces. A higher Cv indicates a greater flow capacity and better energy efficiency, as less pressure is lost across the valve.
Pressure Drop and Flow Coefficient (Cv)
Both gate and ball valves are valued for their low flow resistance when fully open. A full-port ball valve achieves a Cv value that closely matches the pipeline’s internal diameter, typically ranging from 0.9 to 1.0 times the pipeline area. Gate valves also provide an unobstructed flow path when the gate is fully retracted into the bonnet, which can result in slightly higher Cv values than ball valves in certain configurations.
However, the Cv behavior changes significantly as the valve begins to close. The Cv of a gate valve decreases much more rapidly than that of a ball valve during the initial stages of closure. This makes gate valves particularly poor for throttling, as the sudden change in flow area creates high-velocity jets that can damage the internal components. Ball valves, conversely, maintain relatively more linear flow characteristics throughout their operating range, although standard versions are still primarily intended for on/off service.
Throttling and Control Limitations
The engineering consensus is that standard gate and ball valves should not be used for steady-state flow regulation. In a gate valve, a partially open gate is subject to vibration and cavitation, which can lead to seat erosion and eventual failure of the seal. Ball valves face similar risks; when partially open, the high-velocity fluid can blast the side of the ball and the internal soft seats, causing rapid degradation. For applications requiring precise modulation, specialized designs such as V-port ball valves or globe valves are required.
| Hydraulic Metric | Gate Valve (Fully Open) | Ball Valve (Fully Open) | Throttling Suitability |
| Pressure Drop | Near-Zero | Minimal | Poor (Vibration/Erosion) |
| Flow Path | Straight-Through | Straight-Through | Turbulence-Prone |
| Very High | Very High | Inconsistent | |
| Flow Characteristic | Non-linear closing | Linear modulation (relative) | Specialized trims needed |
Sealing Technologies and Material Selection
Sealing performance is arguably the most critical factor in valve selection, especially when handling hazardous, high-pressure, or abrasive fluids. The sealing mechanism determines the valve’s “tightness” and its resilience to environmental stress.
Soft Seats vs. Metal Seats
Ball valves typically utilize resilient or “soft” seats made from polymers such as PTFE (Teflon), RPTFE, PEEK, or Devlon V. These materials deform slightly under pressure to create a “bubble-tight” or zero-leakage seal against the polished surface of the ball. This makes ball valves the preferred choice for natural gas, chemical, and pharmaceutical applications where even minor leaks are unacceptable.
Gate valves often employ metal-to-metal seating, where the wedge and seats are made of stainless steel or hard-faced alloys like Stellite to resist wear and high temperatures. While metal seats can withstand temperatures exceeding 1000 °F, they are more prone to “trace” leakage than soft seats. High-performance ball valves can also be designed with metal seats for severe service, but they often require precision grinding and lapping to achieve reliable sealing.
Fire-Safe Design Standards
In the oil and gas industry, valves must be “fire-safe,” meaning they can maintain a seal even after their primary soft components have been destroyed by fire.
- API 607: Primarily tests soft-seated quarter-turn valves (ball and butterfly). It ensures that after the soft seats melt, the valve can still achieve a backup metal-to-metal seal to contain the fluid.
- API 6FA: A more stringent standard for pipeline valves (API 6D designs), including both soft and metal-seated gate and ball valves. It involves longer fire exposure and evaluates both internal and external leakage under higher pressure.
Seat Effect and Cavity Management (SPE vs. DPE)
For trunnion-mounted ball valves, the way seats respond to pressure is a critical technical detail.
- Single Piston Effect (SPE): These are self-relieving seats. If the pressure in the valve cavity (the space between the ball and the body) increases due to thermal expansion, the SPE seats will “pop off” the ball and vent the excess pressure back into the pipeline.
- Double Piston Effect (DPE): These are bidirectional seats that seal against pressure from both the pipeline and the cavity. While DPE provides a redundant seal (if the upstream seat fails, the downstream seat still isolates), it does not self-relieve. DPE valves require an external relief valve to prevent the body from over-pressurizing.
Operational Dynamics and Actuation
The choice between ball valve vs gate valve significantly impacts the automation strategy and the risk of hydraulic surges in the system.
Operating Speed and Water Hammer
The rapid quarter-turn action of a ball valve allows for fast shutoff, which is critical for emergency systems but can cause “water hammer”—a pressure surge that can damage pipes and fittings. Gate valves, requiring multiple rotations to close, operate slowly and gradually, which minimizes the risk of water hammer and is often preferred for large-diameter water mains.
Torque Requirements for Actuator Sizing
The torque required to operate a valve determines the size and cost of the actuator. Trunnion-mounted ball valves generally have lower operating torque than gate valves of the same pressure class because the ball is fixed and the fluid pressure loads are absorbed by the trunnion bearings rather than the seats. Gate valves must overcome high friction as the gate is pushed against the downstream seat, often necessitating larger, more expensive multi-turn actuators.
| Parameter | Gate Valve | Ball Valve |
| Actuator Type | Multi-turn (Linear) | Quarter-turn (Rotary) |
| Water Hammer Risk | Low | High |
| Typical Torque | High (Friction-based) | Lower (Trunnion-mounted) |
| Speed of Response | Minutes | Seconds |
| Automation Complexity | Moderate | Low |
Maintenance, Reliability, and Lifecycle Cost
The financial viability of a valve selection is determined not just by the initial purchase price (CAPEX) but by the total cost of ownership (TCO) over its service life, including maintenance and energy losses (OPEX).
Maintenance Philosophy and Reliability
Ball valves are often considered “maintenance-free” in many standard applications because their simple design has fewer moving parts exposed to the environment. Their rotary motion minimizes wear on the stem packing, which is a common leak point in linear valves. Gate valves, however, require regular inspection and maintenance, including periodic lubrication of the stem and replacement of the packing to prevent leakage.
A significant failure mode for gate valves is the accumulation of sediment in the bottom pocket, which can prevent the gate from fully closing. Ball valves are less prone to this issue but can suffer from “sticking” if left in the same position for long periods, especially in high-temperature or corrosive environments.
Total Cost of Ownership (TCO) Analysis
For large-diameter pipelines, gate valves typically offer a 20-30% lower initial cost compared to ball valves. This makes them an attractive option for projects with tight initial budgets. However, over a 10-year lifecycle in applications with frequent cycling, ball valves often demonstrate a 40-50% lower TCO. This long-term value is driven by fewer repairs, longer service life, and lower automation costs. Furthermore, the energy savings from lower pressure drops in full-port ball valves can amount to thousands of dollars annually in large industrial systems.
| Cost Category | Gate Valve | Ball Valve |
| Initial CAPEX (Small Pipe) | Lower | Higher |
| Initial CAPEX (Large Pipe) | Significantly Lower | Significantly Higher |
| Annual OPEX (Maintenance) | High | Low |
| Expected Lifespan (Frequent Use) | 5-10 Years | 10-20+ Years |
| TCO Over 10 Years | Higher | Lower |
Application-Specific Recommendations
Industrial sectors have developed distinct preferences for valve types based on operational experience and media characteristics.
Oil and Gas Transmission
The industry standard for natural gas transmission is the API 6D trunnion-mounted ball valve. Its full-bore design, rapid shutoff capability, and bubble-tight sealing make it ideal for protecting long-distance pipelines. Gate valves (specifically API 600) are more common in refinery units where high-temperature hydrocarbons and steam are processed at high pressures.
Municipal Water and Utility Systems
Gate valves are the preferred solution for water distribution mains. Their low flow resistance and gradual operation are perfect for the massive diameters and relatively infrequent operation characteristic of utility networks. In residential and commercial plumbing, ball valves are increasingly used for branch lines and isolation points because of their reliability and ease of use for non-technical personnel.
Mining and Slurry Isolation
Gate valves, particularly through-conduit slab designs or knife gate valves, are often superior for handling slurries and fluids containing suspended solids. Their straight-through path and ability to cut through solids provide better isolation in mining tailings and power plant ash systems. Ball valves can be used for slurries if designed with metal seats and specialized wiping mechanisms, but they are generally more susceptible to clogging if the media is thick.
Chemical and Corrosive Processing
Ball valves dominate the chemical sector due to the wide availability of corrosion-resistant materials and their superior fugitive emission performance. Stainless steel and exotic alloy ball valves (such as Duplex or Inconel) provide long service lives in the presence of aggressive acids and bases.
Dimensional Standards and Interchangeability
For engineers managing existing facilities, “face-to-face” dimensions are critical for ensuring that a new valve fits into an established piping system.
ASME B16.10: The Dimensional Master
ASME B16.10 standardizes the distance between the two gasket sealing surfaces of a valve’s flanges. This ensures that a Class 150 2-inch gate valve from any manufacturer can be replaced by another of the same size and rating. Interestingly, a 2-inch gate valve and a 2-inch ball valve often share the same 178 mm (7-inch) face-to-face dimension, allowing for a technology upgrade without modifying the pipeline. However, ball valves are available in both “short” and “long” patterns, and global compatibility should always be verified against the manufacturer’s data sheet.
| Nominal Size (NPS) | Gate Valve Face-to-Face (mm) | Ball Valve Face-to-Face (mm) | Globe Valve Face-to-Face (mm) |
| 2″ (Class 150) | 178 | 178 | 216 |
| 4″ (Class 150) | 229 | 229 | 292 |
| 6″ (Class 150) | 267 | 267 | 406 |
| 8″ (Class 150) | 292 | 292 | 495 |
Future Trends: Digitalization and Sustainability
The valve industry is entering a new era shaped by ESG (Environmental, Social, and Governance) targets and industrial automation.
Fugitive Emission Control
Reducing the leak of volatile organic compounds (VOCs) from valve stems is a top priority for global chemical and oil companies. Ball valves, with their rotary stems, are inherently easier to seal against fugitive emissions than the linear stems of gate valves, which “pull” media through the packing as they move. New seal designs, such as chevron-style packing and live-loading, are now being integrated into both valve types to meet ISO 15848 standards.
Smart Valves and Remote Monitoring
The integration of sensors into valve actuators allows for real-time tracking of valve performance, including torque trends and seal leakage. These “smart valves” are essential for predictive maintenance in remote pipeline sections and high-risk chemical plants. This trend favors ball valves, as their low torque and quarter-turn action are naturally compatible with the precision feedback systems of advanced electronic actuators.
Concluding Engineering Assessment
The selection between a gate valve and a ball valve is not a matter of identifying a “better” valve, but rather the “right” valve for the specific operating environment.
Gate valves remain the industry standard for large-diameter bulk isolation in water systems and high-pressure refinery utilities (API 600) where slow, steady operation is required to protect the infrastructure. Their lower initial CAPEX in large sizes and robustness in high-temperature service ensure their continued relevance in heavy industry.
Ball valves represent the future of efficient, automated, and leak-free fluid control. Their superior TCO, rapid response, and bubble-tight sealing make them the first choice for natural gas pipelines (API 6D), chemical processing, and energy transition projects such as LNG and hydrogen transport. As the industry moves toward zero-emission and digitally-integrated systems, the ball valve’s technical advantages—particularly in fugitive emission control and actuation—will likely continue to drive its market share expansion.
Engineers and procurement specialists must weigh these technical factors against their project’s lifecycle goals, ensuring that the chosen isolation technology provides the necessary balance of performance, safety, and economic value.